We use our own and third-party cookies to improve our services. If you continue browsing, we will consider that you accept this use. Read More

OK

English-US
  • Spanish-Latin America
  • Japanese-JP
  • Chinese
  • Europe
  • Português-BR

Tech Support

(888) 598-9901
Hours: Mon-Fri 8AM-8PM EST

E-mail

nep-usa@site_ea168614-f5f4-4298-bd5b-880b4cf8d99d

How to Choose Butt Fusion Accessories for PE Pipe Projects?

Choosing the right Butt Fusion Accessories can determine whether a PE pipe joint performs reliably for decades. The decision involves more than selecting clamps, heaters, or facing tools from a catalogue. Each accessory must match the pipe diameter, wall thickness, resin type, fusion machine, and jobsite conditions.

Tony Radoszewski, former president of the Plastics Pipe Institute, has emphasized, “Properly joining polyethylene pipe is essential to achieving the system’s full performance.” That principle applies directly to accessory selection. A misaligned pipe can create uneven heating. A worn facer can leave ridges on the pipe ends. A heater with unstable temperature control may produce a joint that looks acceptable but remains weak internally.

Start with the pipe data.

Check outside diameter, SDR, pressure rating, and manufacturer requirements. Confirm that the machine can hold the pipe securely without crushing it. Select inserts and clamps that support the pipe evenly. Inspect the facer blades before every project. Clean the heater surface and verify its temperature with a calibrated device, not only the machine display.

Standards such as ASTM F2620 and ISO 21307 provide useful process guidance, but they do not replace the equipment manufacturer’s instructions. Site conditions matter too. Mud, wind, rain, and limited working space can change the accessory requirements.

A perfect checklist does not exist. I have seen teams choose expensive accessories that were poorly maintained. That mistake is easy to repeat. The better approach combines proven standards, operator experience, documented inspections, and honest attention to small details. Good Butt Fusion Accessories should make correct fusion easier, more repeatable, and easier to verify.
How to Choose Butt Fusion Accessories for PE Pipe Projects?

Understanding Butt Fusion Accessories and Their Roles

How to Choose Butt Fusion Accessories for PE Pipe Projects?

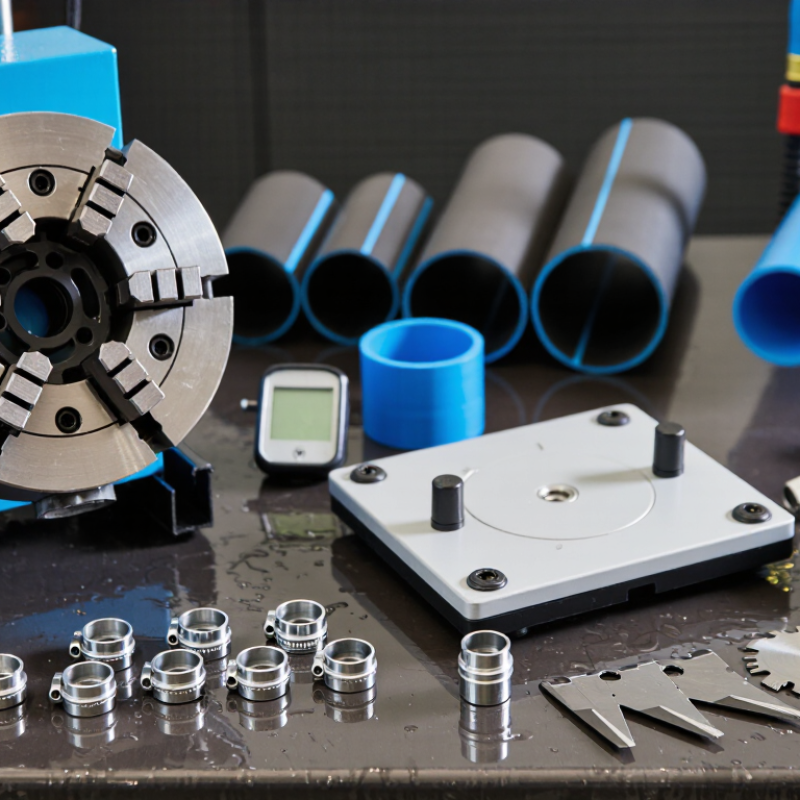
Butt fusion accessories determine whether a PE joint is stable, aligned, and traceable. The main tools include a fusion machine, clamps, facer, heater plate, temperature gauge, and data recorder. Each accessory has a specific role. Clamps hold pipe ends firmly. The facer creates square, parallel surfaces. The heater softens the pipe ends evenly. Without accurate alignment, even good pipe can produce a weak joint.

ASTM F2620 specifies heater surface temperatures between 204°C and 232°C for polyethylene butt fusion. The Plastics Pipe Institute’s Handbook of Polyethylene Pipe explains that a properly prepared fusion joint can achieve strength comparable to the pipe itself. Select accessories according to pipe diameter, SDR, wall thickness, and jobsite conditions. A lightweight machine may suit small service lines, but large-diameter pipe needs stronger hydraulic clamping. Field records should include fusion time, pressure, temperature, and operator details. Small records matter later.

Tips: Check the facer blades before work. Confirm heater temperature with an independent thermometer. Keep dust away from scraped pipe ends. A shiny surface is not always a clean surface. I have seen crews trust machine displays too quickly. That deserves a second check. Also, do not choose accessories only by purchase price. Poor alignment creates rework, delays, and uncertain quality. A simple bead inspection, matched with recorded parameters, gives technicians practical evidence.

Assessing PE Pipe Specifications and Project Requirements

How to Choose Butt Fusion Accessories for PE Pipe Projects?

Choosing butt fusion accessories starts with the pipe, not the equipment catalogue. Confirm the pipe’s outside diameter, wall thickness, SDR, resin type, and pressure class. These details determine suitable clamps, facing tools, heater plates, and reducing inserts. A mismatch can create uneven alignment or incomplete fusion.

Review the project conditions carefully. Trench work may require compact tools, while large-diameter lines need stronger clamps and lifting support. Check ambient temperature, wind exposure, available power, and workspace clearance. Cold weather can affect heating time. Dust and moisture can also reduce joint quality. Use calibrated temperature gauges and follow the approved fusion procedure.

A reliable selection also considers inspection needs. Data recording, pressure gauges, and visual inspection tools can help verify each joint. Operators should understand the applicable standards and receive practical training. Field inspections often reveal a simple mistake: the correct tool was chosen, but the pipe was not properly restrained. That detail matters.

Do not trust assumptions.

Project drawings may contain outdated pipe information. Recheck samples, measure the pipe, and confirm tolerances before mobilization. In practice, even a careful checklist can miss site-specific problems. I would leave room for review after the first trial fusion, especially when the resin, pipe dimensions, or weather differ from earlier work.

How to Choose Butt Fusion Accessories for PE Pipe Projects?

Assess the pipe outside diameter and SDR before selecting butt fusion accessories. Larger diameters require a wider clamping range, greater facing capacity, and properly sized reducing inserts. Wall thickness is calculated as nominal outside diameter divided by twice the SDR value.

Matching Heating, Clamping, and Trimming Tools to Pipe Sizes

Choosing butt fusion accessories starts with the pipe’s actual outside diameter, not its label alone. Measure the pipe and check its SDR, wall thickness, and polyethylene grade. Heating plates must cover the full fusion area evenly. An undersized plate creates cold edges and weak joints. An oversized plate may heat unnecessarily large surfaces and slow the work.

Clamping tools should match the pipe range and hold it without distortion. Select inserts that support the pipe evenly, especially when joining thin-wall sections. The clamps must close smoothly and keep both pipe ends aligned during heating and cooling. Small alignment errors can remain hidden until pressure testing. They should not.

The trimming tool, or facer, also needs enough capacity for the pipe diameter. Its blades should produce flat, parallel ends without tearing the polyethylene. Check blade sharpness before every shift. A clean facing cut reduces gaps between the pipe ends. In dusty conditions, wipe the machine and pipe surfaces before setup. Field crews sometimes focus too much on heating temperature and overlook clamping pressure. That is a costly habit. Accessory selection should also consider transport, power supply, workspace, and operator training. A tool that matches the diameter but cannot fit safely on site is still the wrong choice.

How to Choose Butt Fusion Accessories for PE Pipe Projects? - Matching Heating, Clamping, and Trimming Tools to Pipe Sizes
Typical Pipe Outside Diameter Range Common Application Recommended Clamping Arrangement Typical Heater Plate Working Diameter Trimming Tool Capacity Heating Tool Temperature Range Key Selection Considerations
20–63 mm
(0.75–2.5 in)
Small service lines, irrigation branches, and low-volume utility connections. Compact manual or hydraulic fusion unit with 2 or 4 self-centering clamps; interchangeable inserts may be required for smaller diameters. Approximately 90–160 mm 20–63 mm 204–232 °C
(400–450 °F)
Choose a machine that provides stable alignment at small diameters. Check that the inserts match the actual pipe outside diameter rather than only the nominal pipe size.
63–160 mm
(2.5–6 in)
Building water services, irrigation mains, and small municipal distribution lines. 4-jaw self-centering clamps with manual or hydraulic closing; use pipe supports to prevent sagging during facing and heating. Approximately 160–250 mm 63–160 mm 204–232 °C
(400–450 °F)
Verify that the clamp stroke can accommodate the pipe and that the facing tool can produce parallel, square pipe ends without excessive material removal.
110–250 mm
(4–10 in)
Water distribution, gas distribution, and industrial utility piping. Hydraulic 4-jaw machine with independent or synchronized clamp movement and a dedicated pipe support stand. Approximately 250–350 mm 110–250 mm 204–232 °C
(400–450 °F)
Hydraulic pressure should be controlled according to the approved fusion procedure. The machine must accommodate the pipe wall thickness and required drag pressure.
160–315 mm
(6–12 in)
Municipal water mains, sewer force mains, and medium-size process piping. Hydraulic 4-jaw or 6-jaw alignment system with adjustable pipe rollers and sufficient carriage travel for the fitting or pipe section. Approximately 315–450 mm 160–315 mm 204–232 °C
(400–450 °F)
Use rigid supports on both sides of the machine. Confirm that the clamps can maintain alignment under the combined effects of pipe weight and drag.
250–450 mm
(10–18 in)
Large municipal pipelines, industrial water systems, and mining or slurry services. Heavy-duty hydraulic 4-jaw or 6-jaw machine with reinforced clamps, long carriage travel, and adjustable roller supports. Approximately 450–600 mm 250–450 mm 204–232 °C
(400–450 °F)
Confirm hydraulic capacity, clamp opening, and heater plate flatness. Large-diameter pipes require careful control of alignment, drag pressure, and cooling time.
355–630 mm
(14–24 in)
Transmission water lines, large sewer systems, industrial plants, and infrastructure projects. Heavy-duty hydraulic machine with wide clamp opening, multi-point support, and a stable lifting or positioning system. Approximately 600–800 mm 355–630 mm 204–232 °C
(400–450 °F)
Check transport and lifting requirements as well as working clearance. The heater should provide uniform surface temperature across the full fusion area.
500–1000 mm
(20–40 in)
Large-diameter water transmission, intake and outfall systems, and specialized industrial pipelines. Heavy-duty hydraulic or remotely operated machine with reinforced 4-jaw or 6-jaw clamps, adjustable supports, and high-capacity carriage movement. Approximately 800–1200 mm 500–1000 mm 204–232 °C
(400–450 °F)
Use a qualified fusion procedure for the specific pipe material, outside diameter, SDR, and wall thickness. Verify heater uniformity, hydraulic pressure control, and adequate cooling restraint.
Technical notes: Butt fusion accessories must be selected by actual pipe outside diameter, material grade, SDR, wall thickness, and the applicable joining procedure. The heater temperature range shown is commonly used for polyethylene butt fusion, but the approved project procedure and equipment manufacturer instructions take precedence. Heating time, bead size, joining pressure, cooling time, and drag compensation are not universal values; they must be determined from the applicable standard or qualified procedure. Typical references include ASTM F2620 and ISO 21307.

Evaluating Compatibility, Quality, Safety, and Site Conditions

Choosing butt fusion accessories for PE pipe projects starts with compatibility. Confirm the pipe’s PE grade, outside diameter, wall thickness, and fusion procedure before selecting heaters, clamps, facing tools, or inserts. ASTM F2620 specifies heater-surface temperatures of 204–232°C for many PE fusion applications. Accessories must maintain that range evenly, not merely display it on a screen. ISO 21307 also identifies different fusion procedures, so one pressure setting cannot suit every project.

Quality appears in small details. Check clamp alignment, facing-blade sharpness, pressure calibration, and non-stick heater coatings. The Plastics Pipe Institute’s Handbook of Polyethylene Pipe links joint reliability to clean surfaces, proper alignment, and controlled heating and pressure. A practical check is simple: inspect the pipe ends under bright light. Dust, moisture, or a narrow scrape can undermine an otherwise skilled weld. It is easy to trust new-looking equipment too quickly.

Safety and site conditions deserve equal weight. On muddy ground, choose stable supports and accessories that keep pipe ends level. In cold or windy weather, use an approved shelter and verify actual interface temperature. Keep cables away from standing water, and allow space for lifting long pipe sections without trapping hands. OSHA excavation guidance treats unsupported trench walls as a serious hazard; fusion accessories cannot compensate for unsafe access. I have seen crews focus on bead appearance while ignoring unstable footing. That judgment needs correction. A neat joint is not proof of a safe installation. PPI technical guidance and the manufacturer’s procedure should be checked together before work begins.

Selecting, Inspecting, and Maintaining the Complete Accessory Set

How to Choose Butt Fusion Accessories for PE Pipe Projects?

Selecting, Inspecting, and Maintaining the Complete Accessory Set

A complete accessory set starts with the pipe, not the toolbox. Confirm diameter, wall thickness, PE grade, pressure class, and fusion procedure. ASTM F2620 and ISO 21307 specify heating, joining, and cooling controls. Their values change with pipe dimensions. A mismatch can create a weak joint before installation begins.

Choose compatible clamps, reducing inserts, facer blades, heater plates, alignment tools, and temperature gauges. Check that each component matches the machine’s size range. Inspect clamp faces for dirt, scoring, or uneven wear. Examine the facer for blunt blades. The heater should show a stable, verified surface temperature. A handheld thermometer helps expose inaccurate built-in displays. Small details matter.

Field experience is less tidy. Dust often enters storage cases, and one missing insert can stop an entire crew. I have learned this the hard way. Record inspection dates, calibration results, cleaning actions, and operator observations. The Plastics Pipe Institute’s polyethylene guidance emphasizes controlled fusion conditions and documented procedures. EPA’s 2023 Drinking Water Infrastructure Needs Survey estimates $625 billion in U.S. drinking-water infrastructure needs over 20 years. Preventing avoidable joint failures protects that investment. World Bank assessments commonly place global non-revenue water near 30–40%, although local conditions vary. A damaged accessory may not cause every leak, but ignoring it is an unnecessary risk. Store heater plates dry, protect facer blades, and replace worn inserts before they distort alignment. Loose records fail too.

Get in touch

Our mission is to develop cutting-edge clean energy technology and provide next-generation solar inverters.

Phone

(888) 598-9901

E-mail

nep-usa@site_ea168614-f5f4-4298-bd5b-880b4cf8d99d