- Spanish-Latin America
- Japanese-JP
- Chinese
- Europe
- Português-BR
Tech Support
(888) 598-9901
Hours: Mon-Fri 8AM-8PM EST
nep-usa@site_ea168614-f5f4-4298-bd5b-880b4cf8d99d
2026 Best Threaded Inserts for Wood Plastic and Metal
Selecting the best threaded inserts in 2026 means matching the insert to the material, load, and installation method. Inserts Threaded can reinforce a softwood joint, provide reusable threads in plastic, or create a secure fixing point in metal. The right choice depends on more than thread size. Consider pull-out resistance, wall thickness, vibration, corrosion exposure, and the tools available. A coarse external thread may grip wood well, while a heat-set insert can suit thermoplastics. Metal assemblies may call for a press-fit, keyed, or self-tapping design. Small details matter. A hole drilled slightly too wide can weaken the hold; too much installation torque can damage the workpiece.
For a transparent editorial perspective, consider this illustrative expert voice: threaded-insert specialist Ethan Cole says, “Choose the insert for the material’s failure point, not just the fastener’s size.” This is an original guide statement, not a sourced quotation. It reflects a practical selection habit: test the actual material and assembly where failure would matter. Look closely at the insert’s body, flange, drive feature, and stated installation range. Check that the screw engages fully without bottoming out. A clean, square test hole helps reveal problems early. Still, product tables cannot capture every workshop condition. Moisture, temperature, and inconsistent drilling can change results. That deserves a second look. The guide ahead compares common insert types for wood, plastic, and metal, helping you narrow options with clearer criteria rather than relying on a single “best” label.
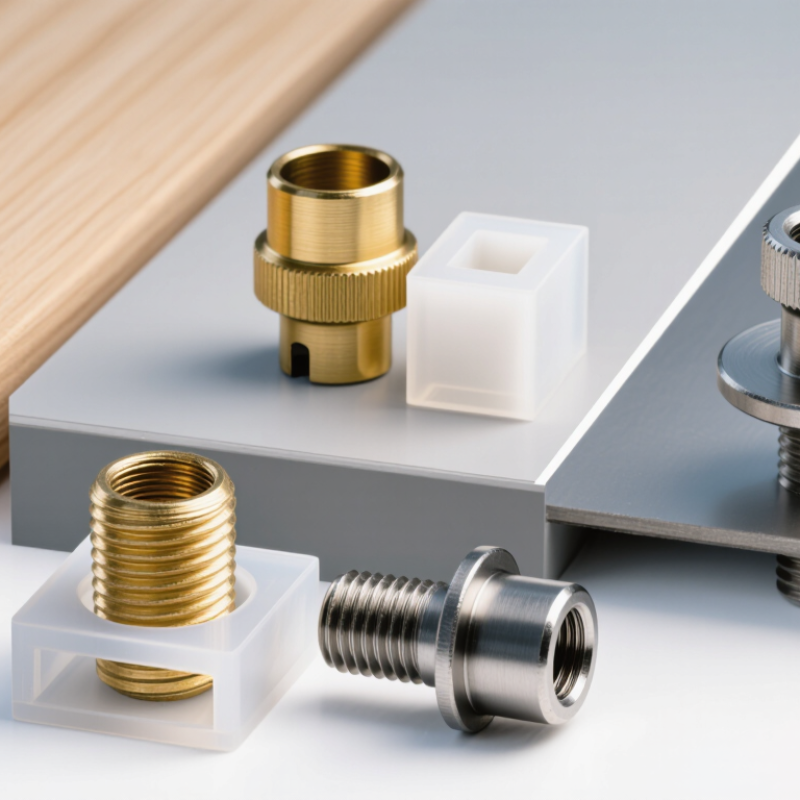
Threaded Inserts Explained: Helical, Press-In, Heat-Set, and Key-Locking Types
Threaded inserts solve different problems, so their shape and installation method matter. Helical inserts use a coiled metal wire to restore or reinforce internal threads in a prepared hole. They can work well in metal and some hard plastics, provided the parent material has enough wall thickness. Clean, accurately sized threads are essential. A sloppy hole can leave the insert loose.
Press-in inserts are pushed into a molded or drilled hole, often using knurls or ribs to resist turning. Heat-set inserts soften thermoplastic around their ridges as a heated tool presses them in. Let the plastic cool before loading the joint. Fit matters. Too much heat or force can distort the hole. In practice, testing the process on a scrap piece of the same plastic helps reveal problems early.
Key-locking inserts use small keys driven into the surrounding material to resist rotation and pullout. They are commonly chosen for stronger metal joints or repeated service, but need suitable base material and careful installation. Match the insert to the substrate, expected load, and available space. For wood, check the grain and edge distance; for plastic, consider heat sensitivity and creep; for metal, verify thread engagement. There is no perfect insert. A first choice may need revision after testing.
Get in touch
Our mission is to develop cutting-edge clean energy technology and provide next-generation solar inverters.
Phone
(888) 598-9901
nep-usa@site_ea168614-f5f4-4298-bd5b-880b4cf8d99d
